How to Test Polyester Spun Yarn Before Bulk Orders
An evidence-based incoming inspection guide covering count, tensile properties, conditioning, package behavior, and lot traceability.
Separate market context from supplier evidence
Incoming-yarn checks work best when they answer a production question. A test report should help a mill decide whether a lot matches the agreed specification and whether observed variation is likely to affect running or fabric quality. It should not rely on a generic phrase such as ‘high strength’ without a method, units, sample identity, and acceptance limit. Tianrun Textile’s product information lists technical and inspection reports and says third-party inspection is supported; buyers should agree in advance which measurements will appear on the report and which party will sample the shipment.
The category is large, but market figures must be interpreted carefully. Textile Exchange estimates global polyester fiber production at 82.5 million tonnes in 2025, compared with 77.7 million tonnes in 2024, equal to 59% of global fiber production. These are fiber-wide production estimates across applications and forms [1]; they are not spun-yarn-only volumes and do not indicate the output, capacity utilization, or sales of any individual supplier. For purchasers, the figures emphasize the scale of polyester supply while reinforcing the need for lot-specific quality records.
Define the lot and sampling plan
Before sampling, freeze the commercial and technical identity of the lot: product code, count convention, ply, color or natural state, package type, lot number, quantity, and date. Use a written specification that identifies the test method, conditioning atmosphere, number of packages tested, and acceptance limits. A sample from one cone may reveal a gross problem, but it cannot represent a large shipment unless the sampling plan supports that conclusion. For incoming inspection, select packages from different positions in the shipment and preserve traceability from package labels to test results.
Measure count and tensile behavior
Linear density is a first check because a count mismatch can affect fabric weight, cover, machine settings, and consumption. ISO 2060 describes determination of yarn linear density from packages by the skein method [3]. A buyer should record the reported value and unit, and compare it with the agreed tolerance rather than assuming the count label alone is sufficient. Confirm whether the supplier uses the same numbering convention as the buyer. A nominal 30s label, for example, is not a substitute for an agreed count system and documented method.
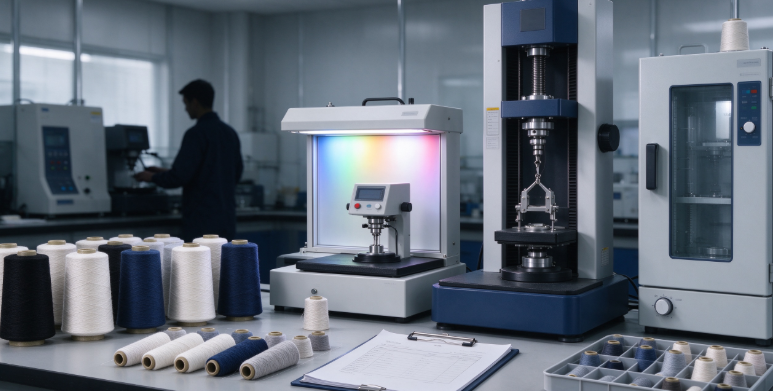
Breaking force and elongation are useful when yarn experiences tension during winding, knitting, weaving, sewing, or a product’s service life. ASTM D2256/D2256M-21 covers tensile properties of monofilament, multifilament, and spun yarns, including single, plied, or cabled yarns within the method’s stated scope. The test result depends on specimen preparation, gauge length, extension rate, pretension, and conditioning. A report should identify the standard and any options used; a buyer should not compare values generated under different test setups as if they were interchangeable.
Check construction and package behavior
Twist, evenness, hairiness, and package build often need separate checks. Twist influences cohesion and handling; unevenness may show up as thick or thin places; hairiness can affect surface appearance, guide friction, and lint. Package density and winding quality affect unwinding tension and interruptions. These measurements are not all contained in the tensile standard. Specify a recognized method that the supplier and buyer can both access, or define a validated internal method with equipment, sample size, and repeatability checks. Do not invent acceptance thresholds from generic internet averages.
Control conditioning and test comparability
Conditioning matters because textile properties can vary with moisture and temperature. ISO 139 defines standard atmospheres for conditioning and testing textile physical and mechanical properties [4], plus an alternative atmosphere that parties may use by agreement. Record the atmosphere and conditioning period in the inspection plan. If the buyer and supplier test samples in materially different conditions, the resulting values may not be comparable. For urgent receiving decisions, a quick visual and machine-unwind check can be useful, but it should not replace a controlled laboratory method when contractual acceptance depends on measured properties.
Use a compact test matrix
A balanced incoming plan combines document review, laboratory measurements, and a short process check. Verify labels and certificates first. Test a risk-based sample for linear density and tensile behavior, then add twist or evenness checks where the end use is sensitive. Unwind the yarn at the intended speed and inspect for sloughing, tangles, package collapse, and inconsistent tension. In a controlled pilot, record the number of ends or courses run, interruptions, and the resulting fabric observations. This produces evidence linked to actual production rather than a stand-alone certificate.
A practical incoming inspection matrix for 100% polyester spun yarn
Check | Useful reference or record | Decision value |
Linear density | ISO 2060:1994; record unit and count system | Confirms count identity against purchase tolerance |
Tensile properties | ASTM D2256/D2256M-21; record force and elongation | Screens strength and extension behavior |
Conditioning | ISO 139:2005; record atmosphere and period | Improves comparability between labs |
Package unwind | Buyer-defined line trial; record speed and stops | Connects package behavior to the actual process |
Lot traceability | Lot, package, date, sample positions | Links results to the shipment |
Test standards define methods, not a universal acceptance value for every textile application. Establish pass limits in the purchase specification before production.
Compare reports and resolve deviations
For a supplier comparison, use the same methods and a common specification. A small difference in a measured result may be within method repeatability; a larger difference can be meaningful only when the sampling and testing protocols are sound. Ask for raw values and lot identity, not just a pass/fail statement. When results miss the target, quarantine the affected material, retain representative packages, and agree on a retest plan before blending, reworking, or returning the lot.
A quality-focused procurement plan avoids claims the data cannot support. The latest public market report provides context for polyester’s scale, while ISO and ASTM methods give a framework for comparable testing. Tianrun’s site presents a 100% polyester staple-spun range from 10s to 60s, with single and plied options, and states that inspection reports and third-party inspection are available. Buyers should still confirm current product specifications, sampling terms, and lot-specific results directly before approving an order.
Frequently Asked Questions
Does a tensile test prove a yarn lot will run well?
No. Tensile results are one part of quality control. Package build, twist, evenness, hairiness, machine settings, and process conditions can also affect running.
What does the 82.5 million tonne figure measure?
Textile Exchange reports global polyester fiber production for 2025 across uses and forms. It is not a spun yarn output figure or an individual supplier’s capacity.
Should a pass/fail certificate be accepted?
It may be useful for routine screening, but buyers should request actual values, methods, units, sample identification, and the agreed acceptance limits for critical properties.
Article body and table: 1110 words